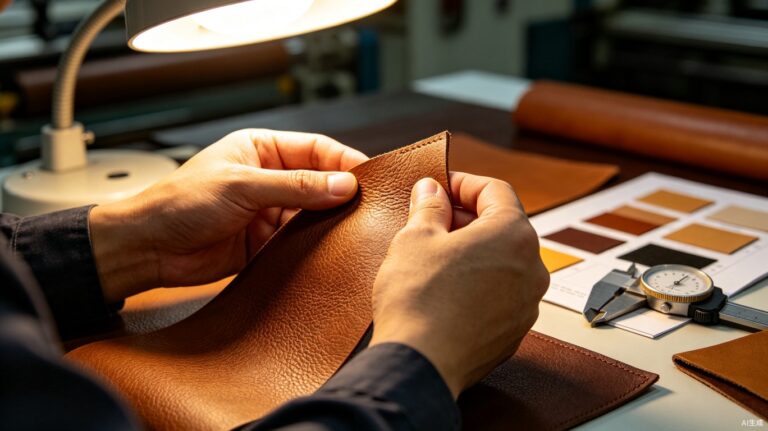
What happens when your product combines leather with foam, metal, plastic, and electronic components? Each material brings its own compliance requirements, supply chain, quality variables, and end-of-life profile. A car seat isn’t just leather — it’s leather + polyurethane foam + steel frame + ABS plastic + electronic heating elements + stitching thread. Each component must pass REACH, ELV Directive, FMVSS 302, and OEM-specific standards independently and in combination. This is the leather & more challenge: managing multi-material product compliance, quality, and cost when each material layer adds risk. For B2B brands, the solution isn’t adding more materials — it’s finding materials that simplify the stack. Silicone leather replaces genuine leather, PU foam coating, and PVC finish layers with a single compliant material that passes REACH, RoHS, FDA, and ISO 10993 simultaneously.

What ‘Leather & More’ Means in B2B Sourcing
In B2B sourcing, “leather & more” refers to multi-material products where leather (or synthetic leather) is one component among several. The “more” includes structural materials (metal, wood, plastic), comfort materials (foam, padding), functional materials (electronics, sensors, heating elements), and finishing materials (thread, adhesives, edge trim). Each material adds a compliance layer, a supply chain dependency, and a quality variable to the final product.
The multi-material product market — where leather or synthetic leather is a primary component — spans automotive interiors ($120B+ annually), furniture ($250B+), medical devices ($50B+), and consumer electronics accessories ($35B+). For brands sourcing these products, the leather & more challenge is that the compliance burden multiplies with each material layer. Genuine leather requires chromium testing. PU foam requires VOC testing. PVC trim requires phthalate testing. ABS plastic requires RoHS testing. Electronic components require conflict mineral documentation. The result: a single car seat carries 8–12 separate compliance test protocols. See our leather goods B2B sourcing guide for the full compliance matrix.
Leather & More Product Categories: 5 Application Segments
| Application Segment | Leather Component | Additional Materials | Compliance Risk | Silicone Alternative |
|---|---|---|---|---|
| Automotive interiors | Seats, door panels, dashboards | Foam, steel, ABS, electronics, thread | REACH + ELV + FMVSS 302 + VOC | Replaces leather + PU coating |
| Furniture | Upholstery, trim, headboards | Foam, wood, metal, adhesives | REACH + formaldehyde + VOC | Replaces leather + PVC trim |
| Medical devices | Chair covers, table pads, cushions | Foam, metal, sensors, electronics | ISO 10993 + REACH + biocompatibility | ISO 10993-5 certified |
| Consumer electronics | Cases, covers, wrist straps | Plastic, metal, electronics, adhesives | RoHS + REACH + Prop 65 | RoHS compliant, heavy-metal-free |
| Fashion/accessories | Bags, wallets, belts, straps | Metal hardware, textile lining, adhesives | REACH + azo dyes + Cr(VI) | Replaces leather + PU coating |

7 Sourcing Challenges in Leather & More Manufacturing
Brands sourcing leather & more products face seven structural challenges that single-material sourcing doesn’t create:
- 1. Compliance stack multiplication: Each material layer requires its own test protocol. A car seat with leather, foam, plastic, and electronics needs 8–12 compliance documents — not one.
- 2. Supply chain coordination: Leather from one supplier, foam from another, plastic from a third, electronics from a fourth. Lead times and quality vary independently across four supply chains.
- 3. Material compatibility: Adhesives that bond leather to foam may not bond leather to plastic. Thermal expansion rates differ across materials, causing delamination under temperature cycling.
- 4. Quality consistency across materials: Leather’s biological variability (20–40% downgrade) affects the final product’s appearance even when other materials are consistent.
- 5. Cost management across layers: Each material layer has its own price volatility. Leather prices track cattle markets; foam prices track oil; metal prices track commodities. Hedging is impossible across four material classes.
- 6. Lead time synchronization: Leather takes 10–30 days to manufacture. Foam takes 3–7 days. Plastic injection takes 1–3 days. The longest lead time — leather — gates the entire production schedule.
- 7. End-of-life recyclability: Multi-material products are difficult to recycle because material separation is labor-intensive. Leather bonded to foam bonded to plastic requires deconstruction before recycling — and often goes to landfill instead.
Silicone Leather: Simplifying Leather & More Supply Chains
Silicone leather addresses the leather & more challenge by consolidating material layers and eliminating compliance risk. Instead of sourcing genuine leather (requiring chromium testing) + PU coating (requiring VOC testing) + PVC trim (requiring phthalate testing), B2B brands source a single material that passes all three compliance dimensions inherently:
- Single compliance profile: REACH compliant, RoHS heavy-metal-free, FDA 21 CFR 177.2600 food-contact certified, ISO 10993-5 biocompatibility certified, near-zero VOC (ISO 16000-6, VDA 277). One material replaces three compliance protocols.
- Consistent quality: Roll-to-roll production with Delta E ≤ 1.0 color consistency eliminates the 20–40% downgrade rate of genuine leather — no biological variability in the multi-material assembly.
- Material compatibility: Silicone’s chemical inertness means it bonds consistently with foam, metal, plastic, and textile substrates — no adhesive compatibility failures.
- Temperature stability: -40°C to 250°C range means silicone leather doesn’t delaminate from adjacent materials under thermal cycling — critical for automotive and outdoor applications.
- End-of-life recyclability: 100% recyclable silicone can be separated from fabric backing and reprocessed — enabling circular economy design for multi-material products.
TOPSUN manufactures silicone leather for leather & more products across automotive, furniture, medical, and consumer electronics applications. With 7 product collections, 100+ textures, unlimited Pantone-matched colors, and custom embossing in 7–10 days, our silicone leather replaces genuine leather and PU/PVC coatings in multi-material assemblies — simplifying compliance, quality, and supply chain coordination. See leather and upholstery sourcing or leather and vinyl comparison.

B2B Brand Checklist for Leather & More Products
- Map every material layer in your product — not just the leather
- Calculate total compliance test cost across all material layers
- Identify which materials carry the highest compliance risk (chromium, VOC, phthalates)
- Check whether silicone leather can replace genuine leather + PU/PVC coatings in one step
- Verify material compatibility at bonding interfaces — especially under thermal cycling
- Assess end-of-life recyclability of the full multi-material assembly
- Request a single-material compliance profile from your silicone leather supplier
The leather & more sourcing challenge is structural: every material layer adds compliance risk, supply chain complexity, and quality variables. Silicone leather’s single-material compliance profile — REACH, RoHS, FDA, ISO 10993, near-zero VOC — eliminates three of the most common compliance protocols in multi-material products. For B2B brands, the simplification is the strategy. See leather and synthetic comparison or leather and PU compliance safety.
Video: TOPSUN silicone leather company profile and multi-material applications
Related reading: leather goods sourcing, leather and vinyl, leather and synthetic comparison, leather and PU compliance