Fabric synthetic leather is not a single material — it is a composite of three engineered layers, and the performance of the finished product depends 90% on how those layers are designed and bonded. A polyester backing fabric that tears at 600 N, coated with a PU polymer that cracks at 25,000 flex cycles, produces a material that fails at 25,000 cycles regardless of the fabric’s strength. Conversely, the same fabric coated with a silicone polymer that survives 200,000 flex cycles produces a material that lasts 8x longer. The fabric synthetic leather industry’s biggest misconception is that performance comes from the coating alone — when in reality, the fabric-coating bond, the base cloth structure, and the coating application method collectively determine whether the material lasts 3 years or 15.
Research data shows PU faux leather achieves 1,008 N breaking force in the warp direction vs 630 N for PVC — a 37.5% difference driven entirely by coating-fabric interaction, not fabric strength alone. Silicone coating achieves even higher composite strength because the polymer penetrates the fabric structure, creating mechanical interlocking rather than surface adhesion.
The Anatomy of Fabric Synthetic Leather: 3 Layers That Determine Performance

Every fabric synthetic leather product — whether PU, PVC, or silicone-based — shares the same three-layer composite architecture. Understanding these layers is the foundation of material specification for B2B buyers:
| Layer | Component | Function | Material Options |
|---|---|---|---|
| 1. Base Fabric | Woven, knitted, or nonwoven textile | Tensile strength, tear resistance, dimensional stability | Polyester, cotton, microfiber, blended |
| 2. Polymer Coating | Synthetic resin applied to fabric surface | Waterproofing, abrasion resistance, surface texture, color | PU, PVC, silicone |
| 3. Surface Finish | Embossing, dyeing, protective treatment | Grain pattern, color, UV protection, stain resistance | Embossing plates, pigments, UV coatings |
Base Fabric Selection: How Backing Material Affects Tensile Strength and Tear Resistance

The base fabric is the structural skeleton of fabric synthetic leather. Its fiber type, weave structure, and weight determine the material’s tensile strength, tear resistance, elongation, and dimensional stability. Here is how the most common backing materials compare:
- Polyester woven fabric — The industry standard for furniture and automotive upholstery. High tensile strength (600–1,200 N warp), excellent dimensional stability, low moisture absorption. Grammage: 150–300 g/m². Best for applications requiring structural rigidity.
- Polyester microfiber — Premium backing for high-end synthetic leather. Fiber diameter of 0.3–0.5 dtex creates a dense, leather-like hand feel. Tensile strength comparable to woven polyester but with superior softness and flexibility. Grammage: 200–400 g/m². Best for premium automotive and luxury accessories.
- Cotton blend — Softer hand feel, higher moisture absorption, lower dimensional stability. Used for fashion accessories where comfort against skin matters more than structural performance. Grammage: 120–250 g/m².
- Nonwoven fabric — Cost-effective backing with moderate strength. Used for budget applications where price is the primary decision factor. Grammage: 80–200 g/m². Lower tear resistance than woven alternatives.
Coating Technology: PU vs PVC vs Silicone — Why the Coating Method Matters More Than the Fabric

While the base fabric provides structural integrity, the coating polymer determines the surface performance that customers actually experience: abrasion resistance, waterproofing, UV stability, and flex endurance. The coating application method — how the polymer is bonded to the fabric — is equally critical:
| Coating Type | Application Method | Bonding Mechanism | Flex Cycles (ISO 5402) | Hydrolysis Resistance |
|---|---|---|---|---|
| PU Coating | Wet coagulation or dry transfer | Surface adhesion | 25,000 | Moderate (ester bond degradation) |
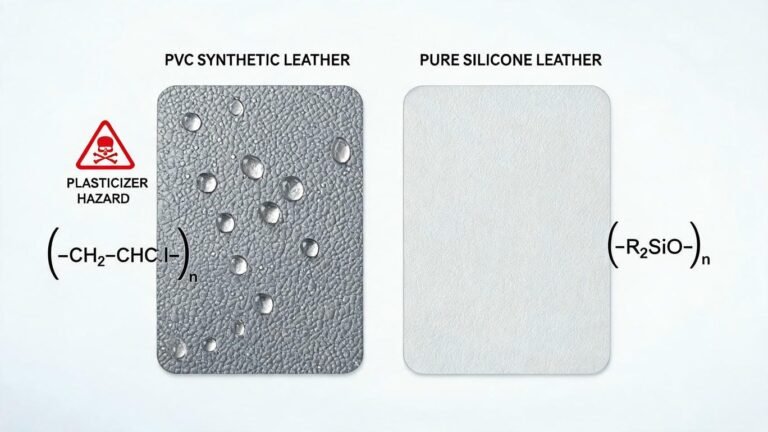
| PVC Coating | Calendering or spread coating | Mechanical lamination | 40,000 | Good (but plasticizer migration) |
| Silicone Coating | Knife-over-roll, 2–3 layers | Molecular penetration + crosslinking | 200,000+ | Excellent (Si-O bond, 452 kJ/mol) |
Flex cycle data per ISO 5402. Hydrolysis resistance reflects polymer chemistry: ester bonds in PU (360 kJ/mol) are susceptible to water molecule attack; silicone Si-O bonds (452 kJ/mol) are chemically inert to hydrolysis.
The bonding mechanism difference is why silicone coating lasts 8x longer than PU. PU coating sits on the fabric surface, held by adhesive force. Silicone coating penetrates the fabric structure during the liquid phase, then crosslinks into a continuous polymer network that is mechanically interlocked with the fibers. You cannot peel silicone coating off the fabric — it becomes part of the fabric structure.
How Fabric-Coating Adhesion Predicts Product Lifespan

The most common failure mode in fabric synthetic leather is not abrasion of the coating surface — it is delamination: the coating separates from the base fabric, creating bubbles, peeling, and structural failure. This is the failure mode that drives the majority of warranty claims for PU and PVC leather products.
Delamination occurs when the adhesive bond between coating and fabric is weaker than the forces acting on the material — flexing, stretching, temperature cycling, and moisture penetration. The ISO 11644 finish adhesion test measures this bond strength, with the threshold for commercial upholstery set at ≥ 4.0 N/10mm.
The three coating technologies handle adhesion differently:
- PU dry transfer coating — Uses a separate adhesive layer between the pre-formed PU film and the fabric. This adhesive is the weakest link — it degrades under heat, moisture, and UV, causing delamination in 3–5 years.
- PVC calendering — The PVC film is mechanically pressed onto the fabric at high temperature. Bond strength is initially high but degrades as plasticizers migrate from PVC into the adhesive interface, softening the bond over 5–8 years.
- Silicone knife-over-roll coating — Liquid silicone is applied directly to the fabric, penetrates the fiber matrix, and crosslinks in place. There is no separate adhesive layer — the coating IS the adhesive. Bond strength does not degrade because there is no interface to degrade. This is why silicone leather does not delaminate, peel, or bubble — ever.
Coating Application Methods: How Process Affects Quality

The method by which the polymer coating is applied to the fabric affects thickness uniformity, surface quality, and production consistency:
- Knife-over-roll coating (TOPSUN’s method) — A precisely gap-controlled blade spreads liquid polymer across the fabric as it passes under a roller. Allows 2–3 layer coating with 0.15–0.50 mm per layer. Thickness tolerance: ±0.02 mm. Produces the most uniform coating with the best fabric penetration.
- Release paper (transfer) coating — Polymer is coated onto embossed release paper, partially dried, then laminated to fabric. The paper is peeled off, leaving the textured surface. Standard for PU leather. Allows texture transfer but creates a surface-only bond (weaker adhesion).
- Calendering — Pre-formed polymer film is pressed onto fabric between heated rollers. Standard for PVC. High production speed but limited fabric penetration and higher thickness variation.
About TOPSUN: Fabric Synthetic Leather Engineered at the Structural Level
TOPSUN manufactures fabric synthetic leather using knife-over-roll silicone coating on polyester and microfiber base fabrics. Our coating process applies 2–3 layers of liquid silicone (0.15–0.50 mm per layer) that penetrate the fabric structure and crosslink into a continuous, integral polymer network. This molecular-level bonding produces materials with 200,000+ Martindale abrasion cycles, 200,000+ flex cycles without cracking, and permanent waterproof performance — because the coating cannot delaminate from the fabric. With ISO 10993, REACH, FDA, and FAR 25.853 certifications, and a production process that controls thickness to ±0.02 mm, TOPSUN delivers fabric synthetic leather where the structural engineering — not marketing claims — defines the performance.
Substrate selection guide — how base fabric choice affects tensile strength, bonding, and flex performance
Fabric Synthetic Leather FAQ
What is the difference between woven and nonwoven base fabric in synthetic leather?
Woven fabrics (typically polyester) have higher tensile strength (600–1,200 N warp) and better dimensional stability, making them suitable for furniture and automotive upholstery. Nonwoven fabrics are cheaper and softer but have lower tear resistance and dimensional stability. For commercial applications, woven polyester is the standard choice; microfiber nonwoven is used for premium applications requiring a leather-like hand feel.
Why does silicone coating outperform PU coating on the same fabric?
The difference is in the bonding mechanism. PU coating is applied as a pre-formed film bonded with a separate adhesive layer — this adhesive interface is where delamination occurs. Silicone coating is applied as a liquid that penetrates the fabric structure and crosslinks in place, creating a continuous polymer network with no separate adhesive layer. There is no interface to fail. Additionally, the Si-O bond (452 kJ/mol) is inherently stronger than the ester bond in PU (360 kJ/mol), providing superior resistance to hydrolysis and UV degradation.
How thick should the coating layer be on fabric synthetic leather?
For furniture upholstery, a total coating thickness of 0.6–1.0 mm (applied in 2–3 layers) is standard. For automotive applications, 1.0–1.2 mm provides better wear resistance. For accessories and fashion items, 0.5–0.8 mm offers the right balance of flexibility and durability. TOPSUN applies coatings in 2–3 layers of 0.15–0.50 mm each, with thickness tolerance of ±0.02 mm for consistent performance across the roll.
Can I specify a custom base fabric for my synthetic leather?
Yes. TOPSUN offers custom base fabric selection including woven polyester (standard and high-density), microfiber, cotton blends, and specialized substrates for specific applications. Custom fabric specifications require a 500-meter MOQ and may add 1–2 weeks to the production lead time for fabric sourcing and testing.
Related resources: Synthetic fabrics for leather production · Factory production tour · Certification gallery · Silicone coated fabric technology
Request Structural Spec Sheet & Cross-Section Samples
Get cross-section samples showing the three-layer structure, full technical data sheet with coating thickness, fabric grammage, and adhesion test results. See the structural engineering difference between silicone and PU fabric synthetic leather firsthand.