Last spring, a design studio in Milan sent us a brief for a custom leather collection: 12 Pantone colors, three distinct textures, and a 0.4mm thickness spec. They’d already been through two suppliers who couldn’t match the colors closer than Delta E 3.5 — visible to the naked eye under showroom lighting. We delivered first-pass approval on 11 of 12 colors. Here’s what made the difference, and why most designer custom leather projects stall at the sampling stage when key specifications go undefined.
The Color Matching Standard That Separates Pros from Amateurs
Color matching is where most custom leather projects go off the rails. The industry default is Delta E 2.0-3.0 — a perceptible difference you can see under neutral daylight. Most suppliers work to this standard because it’s cheaper: fewer color trials, less pigment waste, faster turnaround. The problem is that Delta E 2.0 shows up brutally under retail lighting, especially when two batches sit side by side on a showroom floor.
Our color lab targets Delta E ≤ 1.0, which is the threshold where the human eye can no longer distinguish between the target and the sample. We mix silicone pigment pastes in small-batch trials, producing three variants: on-target, slightly lighter, and slightly deeper. This gives the design team a range to evaluate under their own lighting conditions. For brands working with Pantone references, we cross-verify against the physical chip and the digital value. The extra round of verification adds 48 hours to sampling but eliminates the rework cycle that costs 2-3 weeks downstream.

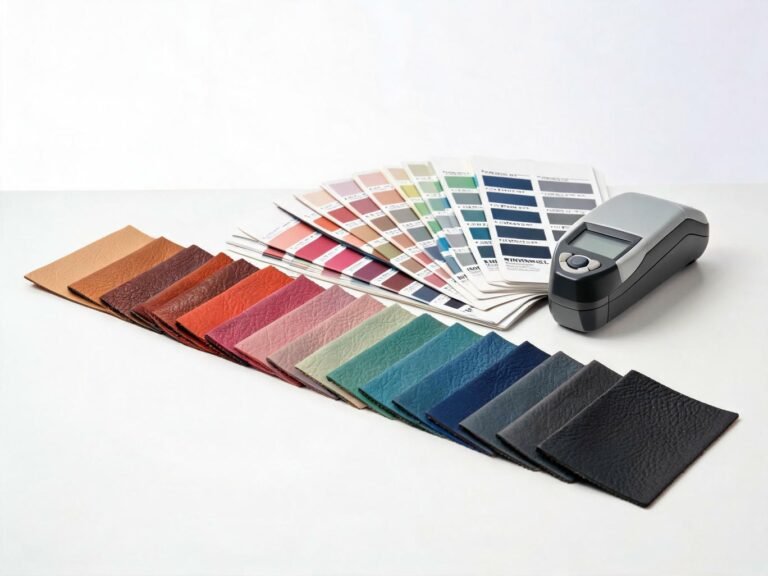
Custom color development starts with a comprehensive swatch library for Pantone reference matching.
Custom Texture and Embossing: What’s Actually Possible
When designers request a “custom texture,” they’re often thinking of the end visual without knowing the engineering behind it. There are four primary methods for creating custom leather surfaces, and each has different cost, detail, and timeline implications:
- Release paper embossing — engraved paper transfers a pattern during coating. Fastest method, 200+ standard patterns available, custom patterns add 10-15 days.
- Laser etching — burns precise geometric or decorative patterns into the surface. Best for logos and fine detail work.
- Perforation — mechanical hole patterns for breathability or aesthetic effect. Adds 2-3 weeks to production.
- Digital printing — full-color graphics on the leather surface. Unlimited design freedom but lower abrasion resistance on the printed layer.
For silicone leather specifically, release paper embossing is the workhorse. The silicone coating takes texture impressions with exceptional fidelity — better than PU, which tends to flatten under heat. We maintain a library of 200+ release papers and can develop custom patterns from a designer’s CAD file in 10-15 days. Learn more about our custom texture design process and how it integrates with your production schedule.

Custom texture samples allow designers to evaluate grain depth, sheen, and tactile response before committing to production.

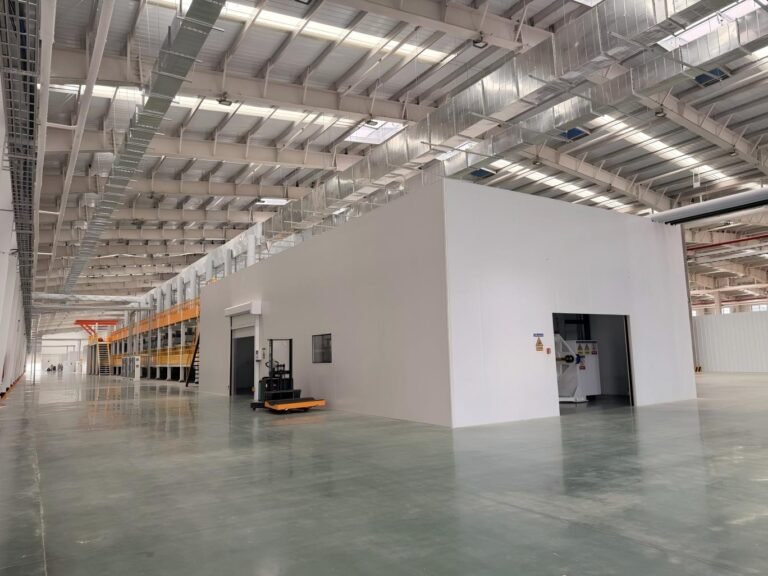
Release paper coating line where custom texture patterns are transferred to the silicone surface during production.
Tolerance and Thickness: The Specs Designer Custom Leather Buyers Forget
Here’s a spec that rarely appears on a design brief but quietly determines production yield: thickness tolerance. If you’re die-cutting panels for bags, phone cases, or furniture components, a thickness variation of ±0.15mm across a roll means some panels will be under-spec and get rejected. That’s wasted material, wasted labor, and delayed delivery.
Our standard thickness tolerance is ±0.05mm — three times tighter than the synthetic leather industry norm of ±0.15mm. We achieve this through in-line thickness monitoring at three points across the web width, with automatic adjustment of the coating knife. For silicone leather production, this precision matters because the material is often specified at thinner gauges (0.4-0.8mm) where small variations have outsized impact on die-cutting yield. A 2% improvement in yield on a 5,000-meter order pays for the spec sheet it was written on.

Color fastness testing ensures custom-matched colors resist fading under UV, abrasion, and chemical exposure.
Designer Custom Leather Production Timeline: What to Expect
The single most common source of friction between designers and leather suppliers is timeline misalignment. Designers expect Amazon-speed; custom leather production has its own rhythm. Here’s what a realistic schedule looks like when you’re specifying custom colors and textures:
- Days 1-3: Color lab trial — pigment formulation and first sample
- Days 4-7: Client review and Delta E verification under their lighting
- Days 8-12: Texture embossing trial if custom pattern is required
- Days 13-15: Final approval sample (FA) produced and shipped
- Days 16-35: Production run for first order (standard custom)
For entirely new texture development requiring a custom engraved roller, add 10-15 days to the front of the schedule. The total from first brief to delivered production runs 25-35 days for standard custom and 35-45 days for new texture development. Our factory production capabilities include dedicated lines for custom runs, which means your order isn’t queued behind bulk standard production.
Delta E ≤ 1.0, ±0.05mm thickness tolerance, and 7-day first sample turnaround are the three specs that separate first-pass approval from three rounds of rework. Get them in writing before you commit.
| Customization Spec | Industry Standard | TOPSUN Standard | Production Impact |
|---|---|---|---|
| Color Matching (Delta E) | 2.0-3.0 | ≤ 1.0 | Eliminates batch-to-batch color disputes |
| Thickness Tolerance | ±0.15mm | ±0.05mm | Higher die-cutting yield, fewer rejects |
| Texture Library | 50-100 patterns | 200+ patterns | Faster selection, less custom development |
| First Sample Turnaround | 14-21 days | 7-10 days | Shorter approval cycle, faster to market |
| Custom Pattern Development | 20-30 days | 10-15 days | Enables exclusive textures for brand identity |
Specifications verified through in-house testing. Delta E measured per CIE Lab color space under D65 illuminant.
See how custom patterns are engineered from CAD file to finished leather surface in our pattern customization process.
Frequently Asked Questions
What’s the minimum order quantity for custom color leather?
Custom color development requires a dedicated pigment formulation and trial run, so the MOQ is typically 500 meters for standard colors and 1,000 meters for entirely new formulations. Sampling before commitment is always available — see our custom leather texture design guide for details on the sampling process.
Can you match a color from a physical sample instead of a Pantone code?
Yes. Our spectrophotometer reads the Lab values from any physical sample — fabric, metal, paper, or existing leather — and we formulate to those values. This is common for brands matching a corporate color or an existing product line. The quality standards for custom production apply the same Delta E ≤ 1.0 threshold regardless of the reference source.
From Brief to Approval: Getting It Right the First Time
Designer custom leather projects succeed when specifications are locked before sampling begins, not after the third round of rework. The five specs that matter most — Delta E target, thickness tolerance, texture method, MOQ, and timeline — should appear on your brief as hard numbers, not aspirational goals. When your supplier can meet Delta E ≤ 1.0, ±0.05mm tolerance, and deliver first samples in 7-10 days, you’ve found a partner who takes your design intent as seriously as you do.
About TOPSUN
TOPSUN engineers custom silicone leather solutions for designers and brand teams who need precise color, texture, and thickness specifications without compromise.
In-house color lab with Delta E ≤ 1.0 matching capability | Custom embossing from 200+ release paper patterns | Thickness tolerance ±0.05mm verified in-line | First-pass sample approval in 7-10 days.